Keilwellenwalzen vs. -schneiden: Faktoren der Verfahrensauswahl — Spline rolling forms teeth by plastic deformation while cutting removes material. The choice affects blank preparation, tooling investment, material flow, achievable geometry and production economics; it should be based on the complete part and quantity rather than a general assumption that one process is always stronger or cheaper.
Für spline rolling vs cuttingDie zuverlässigste Spezifikation ist diejenige, die von Konstrukteur, Käufer, Hersteller und Prüfer gleichermaßen interpretiert werden kann. Die folgende Diskussion konzentriert sich auf messbare Zeichnungseingaben, Montagebedingungen und praktische Prüfungen anstatt auf universelle Drehmoment-, Passungs- oder Lebensdauerangaben, die ohne vollständige Geometrie- und Belastungsdaten nicht ermittelt werden können.
Material Flow In Rolling
Material Flow In Rolling Die Auswahl sollte anhand von Belastung, Querschnittsgröße, Härtungsverhalten, Stoßbeanspruchung, Verschleißanforderungen und dem geplanten Fertigungsweg erfolgen. Werkstoffgüte und Wärmebehandlung bilden eine gemeinsame Entscheidung; ein höher legierter Stahl ist nicht automatisch die bessere Wahl, wenn die Beanspruchung und Geometrie dies nicht erfordern.
The drawing should state the required material designation and final condition. If a material substitution is allowed, define the properties or approval process that control it. For shafts with several diameters or integrated gears, also consider how the heat-treatment route affects straightness and later finishing. For this topic, connect that decision to the mating component and the drawing revision used for the RFQ. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
Cutting As Material Removal
Cutting As Material Removal Die Auswahl sollte anhand von Belastung, Querschnittsgröße, Härtungsverhalten, Stoßbeanspruchung, Verschleißanforderungen und dem geplanten Fertigungsweg erfolgen. Werkstoffgüte und Wärmebehandlung bilden eine gemeinsame Entscheidung; ein höher legierter Stahl ist nicht automatisch die bessere Wahl, wenn die Beanspruchung und Geometrie dies nicht erfordern.
The drawing should state the required material designation and final condition. If a material substitution is allowed, define the properties or approval process that control it. For shafts with several diameters or integrated gears, also consider how the heat-treatment route affects straightness and later finishing. In this review, the useful acceptance criterion is the one that can be traced to a functional drawing characteristic. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
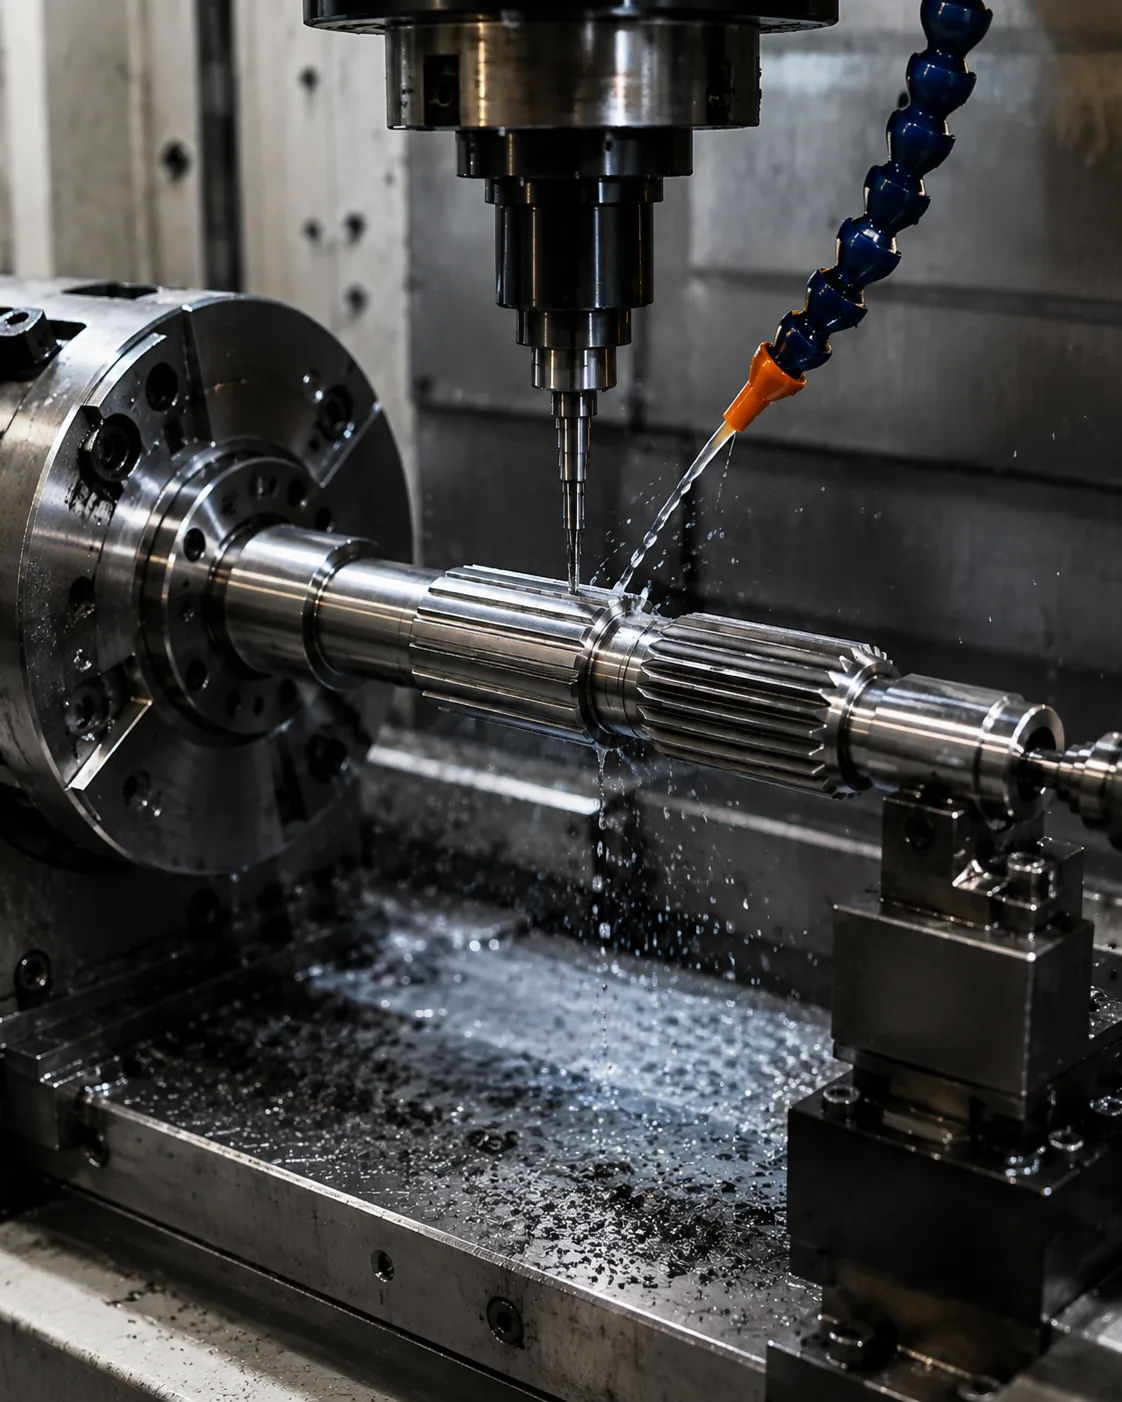
Blank Diameter Control
Blank Diameter Control should be reviewed in the context of spline rolling vs cutting. Identify the mating component, operating function and drawing feature that this decision controls. The requirement should be measurable and connected to fit, torque transfer, alignment, wear or another defined assembly need.
Consider the decision together with material condition, manufacturing sequence and inspection access. If the part is a replacement, compare unworn geometry and the mating member instead of copying damage. For new designs, keep open process choices flexible unless a specific process is itself required by the design. For repeat work, keep the same datum and measurement basis unless the assembly requirement changes. For Spline Rolling vs Cutting: Process Selection Factors, record the resulting requirement on the drawing or purchase specification so it remains consistent on repeat orders.
Grain Flow And Surface Finish
Grain Flow And Surface Finish should be tied to function. Spline flanks, bearing seats, seal lands and pilot diameters do not necessarily need the same finish, and a cosmetic polished surface is not a substitute for a measurable roughness requirement.
Call out roughness locally where it affects friction, wear, sealing, fit or measurement repeatability. For internal features, confirm that the chosen inspection method can access the surface. If finishing occurs after heat treatment, include enough stock and datum control for the final operation.
Tooling Cost And Production Volume
Tooling Cost And Production Volume Die Fertigungsentscheidung hängt von der Zahngeometrie, der Zugänglichkeit, dem Materialzustand, dem Produktionsvolumen und der geforderten Genauigkeit ab. Außen- und Innenverzahnungen erfordern oft unterschiedliche Werkzeugstrategien, und Absätze oder angrenzende Durchmesser können die Werkzeugzufahrt einschränken.
Definieren Sie zunächst die fertige Zahngeometrie und das Abnahmeverfahren. Wählen Sie anschließend einen geeigneten Prozess, der diese effizient umsetzen kann. Die Wärmebehandlung kann die Reihenfolge beeinflussen: Vorschleifen oder Weichschneiden kann vor dem Härten erfolgen, während Schleifen oder andere Hartbearbeitungsverfahren für Bereiche reserviert sind, die nach thermischer Verformung korrigiert werden müssen. Ändern sich die Anforderungen oder das Gegenstück, überprüfen Sie diesen Punkt erneut, anstatt die bisherige Annahme beizubehalten.
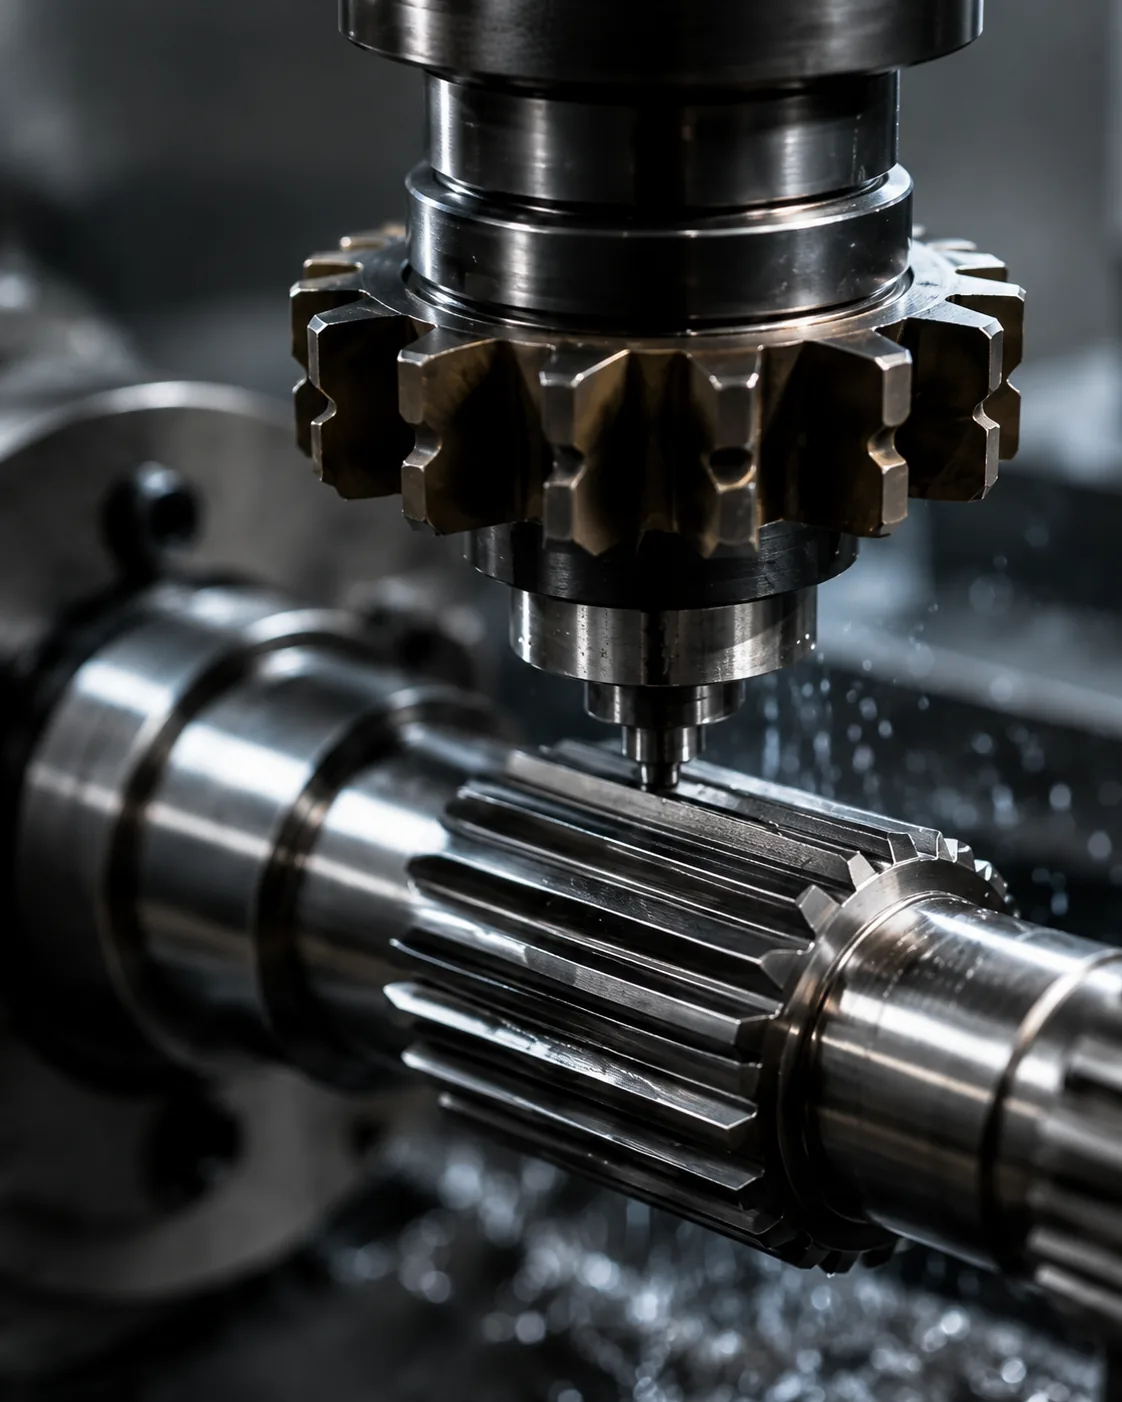
Geometry Limits
Geometry Limits should be reviewed in the context of spline rolling vs cutting. Identify the mating component, operating function and drawing feature that this decision controls. The requirement should be measurable and connected to fit, torque transfer, alignment, wear or another defined assembly need.
Consider the decision together with material condition, manufacturing sequence and inspection access. If the part is a replacement, compare unworn geometry and the mating member instead of copying damage. For new designs, keep open process choices flexible unless a specific process is itself required by the design. For this topic, connect that decision to the mating component and the drawing revision used for the RFQ. For Spline Rolling vs Cutting: Process Selection Factors, record the resulting requirement on the drawing or purchase specification so it remains consistent on repeat orders.
Eine praktische Wiederholungssequenz
A practical review sequence starts with the mating component and torque path, then confirms tooth system, engagement and the shaft features that locate the connection. Next define material and heat treatment, functional finishes and any runout or position requirements. In this review, the useful acceptance criterion is the one that can be traced to a functional drawing characteristic. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
Finish by agreeing the inspection method, quantity and first-article documentation. This order prevents process or tolerance decisions from being made before the functional interface is understood and makes quotations easier to compare because the same design inputs are presented to each supplier. For repeat work, keep the same datum and measurement basis unless the assembly requirement changes. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
Wärmebehandlungssequenz
Wärmebehandlungssequenz Die Härte beeinflusst Verschleißfestigkeit, Ermüdungsverhalten, Verformung und die Reihenfolge der Endbearbeitung. Aufkohlen, Induktionshärten und Anlassen erzeugen unterschiedliche Materialzustände und sollten daher nicht als austauschbare Verfahren zur Erreichung eines bestimmten Härtewerts betrachtet werden.
Specify hardness with a location and, where required, case depth or core condition. If heat treatment can change straightness or feature relationship, plan the datum recovery and final inspection after the thermal process. Critical journals or tooth surfaces may need finish stock when tight tolerances must be restored. When the duty or mating member changes, revisit this point instead of carrying the previous assumption forward. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
Inspection And Qualification
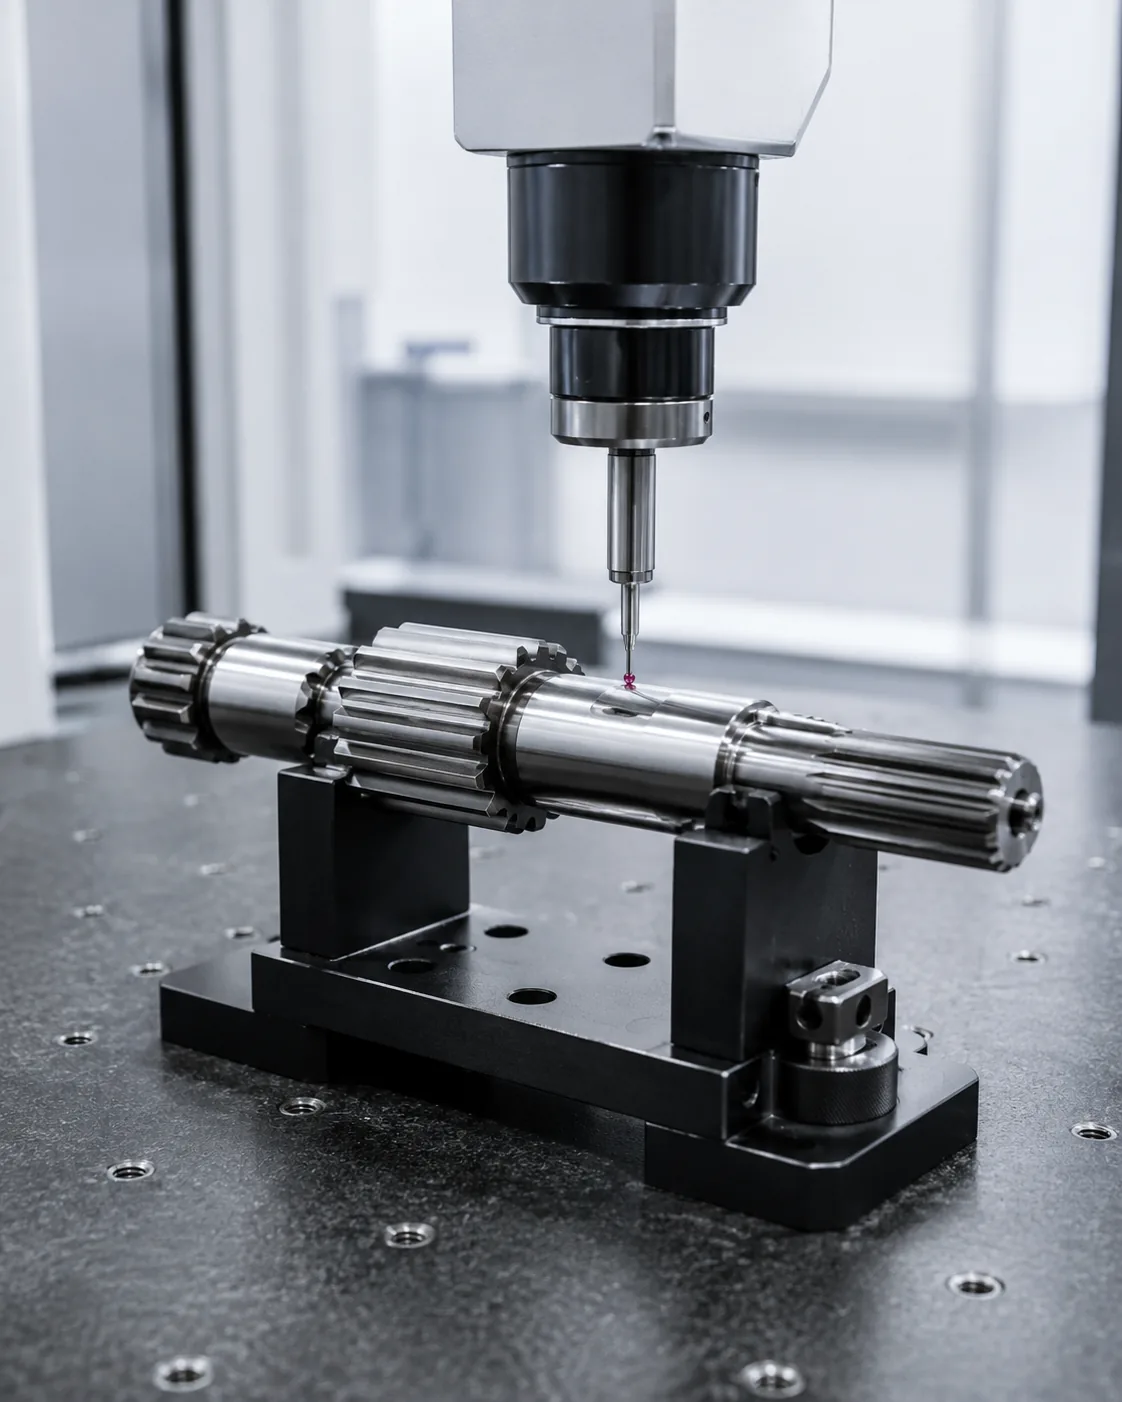
Inspection And Qualification Es sollte eine Methode verwendet werden, die die Zeichnungseigenschaften direkt oder funktional misst. Funktionale Lehren, analytische Zahnmessung, KMG-Prüfung, Spannweitenmessungen und Messungen über Stifte oder Kugeln beantworten unterschiedliche Fragestellungen und sind nicht standardmäßig austauschbar.
Agree the method before production when tolerance is tight or when customer and supplier use different equipment. Control temperature, cleanliness and gage calibration for repeatability. The inspection report should identify the drawing revision and datum setup so later lots can be compared on the same basis. For this topic, connect that decision to the mating component and the drawing revision used for the RFQ. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
Häufige Fehler, die es zu vermeiden gilt
Common errors in spline rolling vs cutting come from treating one nominal value as if it defines the complete interface. Missing pressure angle, unclear datums, copied wear dimensions, unspecified hardness location and mismatched inspection methods can all create parts that look correct on paper but do not assemble consistently.
A better review starts with the mating pair, identifies the load path and locating features, then connects geometry, material condition and inspection to those functions. Close open questions on the drawing before production and retain the agreed interpretation with the revision for repeat orders. In this review, the useful acceptance criterion is the one that can be traced to a functional drawing characteristic. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
Entscheidungszusammenfassung
| Entscheidungsbereich | Was zu bestätigen ist | Warum es wichtig ist |
|---|---|---|
| Paarungsgeometrie | Zahnsystem, Durchmesser, Eingriff und Passung | Kontrollierkompatibilität und Flankenkontakt |
| Standort | Bezugspunkte, Journale, Schultern und Auslauf | Steuert die Ausrichtung in der Baugruppe |
| Materialzustand | Güteklasse, Wärmebehandlung, Härte und Oberflächenbeschaffenheit | Definiert den fertigen mechanischen Zustand und den Verschleißzustand |
| Pflicht | Drehmoment, Geschwindigkeit, Stoß, Bewegung und Umgebung | Verknüpft die Teiledefinition mit den Betriebsbedingungen |
| Inspektion | Kontrollierte Merkmale und Messmethode | Gewährleistet einheitliche Akzeptanz zwischen Lieferant und Käufer |
Checkliste für Spezifikationen
- Gegenstück und äußere/innere Zahnausrichtung
- Modul oder Teilungssystem, Zähnezahl, Eingriffswinkel und Außen-/Kerndurchmesser
- Effektives Einrasten, Passung oder Toleranzgrundlage und gegebenenfalls axiale Bewegung
- Werkstoff, Wärmebehandlung, Härtebereich und funktionelle Oberflächenbeschaffenheit
- Bezugspunkte, Lager- oder Pilotdurchmesser, Rundlauf- und axiale Lageanforderungen
- Drehmoment, Drehzahl, Stoß- oder Wechsellast, Schmierung und Betriebsumgebung
- Mengen-, Erstmuster- und vereinbarte Prüfdokumentation
Verwenden Sie die Produktpalette an Keilwellen um die verfügbaren Konfigurationen und die Checkliste für Angebotsanfragen to prepare a complete enquiry. For repeat work, keep the same datum and measurement basis unless the assembly requirement changes. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
Engineering worksheet for spline rolling vs cutting
Verwenden Sie dieses Arbeitsblatt, um es umzudrehen Keilwellenwalzen vs. -schneiden: Faktoren der Verfahrensauswahl in Entscheidungen, die in einer Zeichnung dargestellt, während der Angebotserstellung überprüft und bei der Erstbemusterung verifiziert werden können. Beginnen Sie mit Material Flow In Rolling Und Cutting As Material RemovalDenn diese beiden Elemente definieren üblicherweise entweder die Geometrie der Passung oder die Materialbeschaffenheit, die der restliche Prozess erfüllen muss. Anschließend überprüfen Blank Diameter Control, Grain Flow And Surface Finish Und Tooling Cost And Production Volume gegenüber der tatsächlichen Baugruppe und nicht als unabhängige Katalogwerte zu behandeln.
For a manufacturing-process decision, start from the finished tooth geometry and access conditions. Note whether the spline is external or internal, through or blind, close to a shoulder, integrated with a gear, or restricted by adjacent diameters. Those constraints influence tool approach, workholding and the practical choice between processes. Production quantity and material condition affect economics, but the drawing characteristic remains the acceptance target. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
Build the inspection handoff around blank diameter control. Define the datum setup, measurement stage and reporting requirement before the first article. Heat treatment can move features relative to each other, so runout, lead, tooth thickness or bore relationships may need to be verified after the final process rather than on a soft-machined blank. Where gages are used, agree what they prove and what analytical checks remain necessary.
Zeichenüberprüfungssequenz
Vor der Produktionsanforderung ist die Zeichnung in der gleichen Reihenfolge zu prüfen, in der die Baugruppe arbeitet: zusammenpassendes Zahnsystem, effektiver Eingriff, Bezugspunkte, angrenzende Zapfen oder Schultern, Werkstoff und Wärmebehandlung, funktionelle Oberflächen und Prüfverfahren. spline rolling vs cuttingDie Reihenfolge ist wichtig, weil spätere Entscheidungen wie die Prozessauswahl oder die Wahl des Messgeräts die Schnittstelle unterstützen und nicht neu definieren sollten.
| Arbeitsblattelement | Frage zur Beantwortung | RFQ-Ausgabe |
|---|---|---|
| Material Flow In Rolling | Welche Baugruppenfunktion wird von diesem Feature gesteuert? | Maß-, Toleranz- oder Passungsbezug |
| Cutting As Material Removal | Welcher Endzustand muss erreicht werden? | Material- / Wärmebehandlungs- / Oberflächenbezeichnung |
| Blank Diameter Control | Wie wird das Merkmal überprüft? | Prüfmethode oder Berichtsvermerk |
| Grain Flow And Surface Finish | Wie verhält sich das gegnerische Mitglied? | Informationen zu Paarungsteilen und deren Verzahnung |
| Tooling Cost And Production Volume | Welches Datum legt den funktionalen Standort fest? | Bezugspunkt und Auslauf |
Übergabe des Beschaffungsprozesses vor dem ersten Artikel
Ein nützliches Einkaufspaket für Keilwellenwalzen vs. -schneiden: Faktoren der Verfahrensauswahl Die 2D-Zeichnung enthält die kontrollierte Zeichnung, die Menge, das Material und den Wärmebehandlungszustand, Informationen zur Passfläche sowie die zu meldenden Abnahmekriterien. Wird ein 3D-Modell bereitgestellt, muss die 2D-Zeichnung weiterhin Toleranzen, Bezugspunkte, Hinweise zur Wärmebehandlung und Prüfanforderungen enthalten. Geben Sie die aktuelle Revision in der Angebotsanfrage an, damit Fertigung und Prüfung nicht mit unterschiedlichen Versionen arbeiten.
When a characteristic is not yet decided, mark it for engineering clarification rather than inserting a convenient value. For spline rolling vs cutting, common open items are engagement, fit, hardness location, runout to an adjacent journal, internal-feature access or the condition of a worn mating component. Resolving those points before first article reduces avoidable rework and makes later repeat orders easier to control.
Checkliste vor der Veröffentlichung
- Confirm material flow in rolling against the actual mating component.
- Confirm cutting as material removal in the finished condition.
- Define how blank diameter control will be inspected.
- Check grain flow and surface finish under the intended assembly condition.
- Relate tooling cost and production volume to the functional datum structure.
- Menge, Revisionsstand und etwaige Dokumentationsanforderungen für das Erstmuster angeben.
- Änderungen bei der Belastung, der Schmierung oder den passenden Verbindungsteilen für Nachbestellungen dokumentieren.
Häufig gestellte Fragen
What should I confirm about material flow in rolling for spline rolling vs cutting?
Relate material flow in rolling to the mating component and the assembly function first. Put the measurable requirement on the controlled drawing, and include the opposite member when compatibility depends on both parts. For Spline Rolling vs Cutting: Process Selection Factors, this prevents a nominal label from replacing the geometry that actually controls fit and torque transfer.
What should I confirm about cutting as material removal for spline rolling vs cutting?
Confirm cutting as material removal in the finished condition, including any material, heat-treatment, surface or dimensional state that can change after processing. If the requirement depends on a location or datum, show that explicitly so production and inspection use the same reference.
What should I confirm about blank diameter control for spline rolling vs cutting?
Choose an inspection method that measures the characteristic named on the drawing. Functional gaging, analytical spline measurement, CMM checks, runout inspection, roughness measurement and hardness testing answer different questions. State which result is required for acceptance rather than requesting a generic inspection report. For Spline Rolling vs Cutting: Process Selection Factors, record the resulting requirement on the drawing or purchase specification so it remains consistent on repeat orders.
What should I confirm about grain flow and surface finish for spline rolling vs cutting?
Check grain flow and surface finish with the real mating part and intended assembly condition. Effective engagement, clearance, axial movement, temperature and wear in a replacement hub can all influence how the connection behaves. A new shaft should not be accepted or rejected from feel alone when a measurable fit requirement is available.
What should I confirm about tooling cost and production volume for spline rolling vs cutting?
Tie tooling cost and production volume to the features that locate rotation in the assembly. The drawing should make the datum reference and any runout or position relationship clear. If heat treatment or finish machining can move the feature, inspect the relationship at the stage that represents the finished part.
Von der technischen Entscheidung bis zur Produktionssteuerung
Once the interface is agreed, translate each functional decision into a drawing characteristic that can be manufactured and inspected. Avoid leaving key relationships only in email notes. Dimensions, datums, heat-treatment conditions and acceptance requirements should be revision-controlled so the production team and inspection team work to the same definition. In this review, the useful acceptance criterion is the one that can be traced to a functional drawing characteristic. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
For first articles, prioritize the characteristics that prove assembly compatibility: tooth geometry, mating fit, relationship to locating journals or shoulders, heat-treatment condition and any critical runout. Record the measurement method together with the result. On repeat orders, using the same datum setup and measurement approach makes trend changes easier to recognize and reduces disputes caused by different inspection interpretations. For repeat work, keep the same datum and measurement basis unless the assembly requirement changes. For Spline Rolling vs Cutting: Process Selection Factors, apply this check to the specific spline rolling vs cutting interface shown on the current drawing.
When the operating duty changes, reopen the engineering review instead of assuming the old specification remains suitable. Higher torque, increased shock, more frequent reversals, different lubrication or a new mating component can change contact and wear even if the nominal spline size stays the same. The drawing should evolve with the actual assembly requirement. When the duty or mating member changes, revisit this point instead of carrying the previous assumption forward. For Spline Rolling vs Cutting: Process Selection Factors, record the resulting requirement on the drawing or purchase specification so it remains consistent on repeat orders.
Bereiten Sie die Angebotsanfrage vor.
- Aktuelle 2D-Zeichnung und Überarbeitung
- Partnerkomponente und Spline-Definition
- Material, Wärmebehandlung und funktionelle Oberflächen
- Drehmoment, Drehzahl, Belastung und Umwelt
- Mengen- und erforderliche Prüfdokumentation
A complete enquiry combines the drawing, mating interface, material condition, duty, quantity and inspection expectations. When these inputs are defined early, suppliers can plan tooling, heat treatment, finishing and measurement around the same functional requirement, reducing clarification cycles before first article. For this topic, connect that decision to the mating component and the drawing revision used for the RFQ. When reviewing spline rolling vs cutting, revisit this point whenever the mating component, material condition or operating duty changes.
Wandeln Sie den Leitfaden in eine Angebotsanfrage um.
Senden Sie die kontrollierte Zeichnung, die Angaben zur Verbindungsschnittstelle, zum Materialzustand und zur Verwendungsart zur technischen Prüfung.
Angebot anfordern